Preventing Condensation Drips, Microbial Growth & Product Loss
Protect chocolate panning, bakeries, meat chilling rooms, and cheese curing cellars with sanitary, washdown-ready moisture control systems.
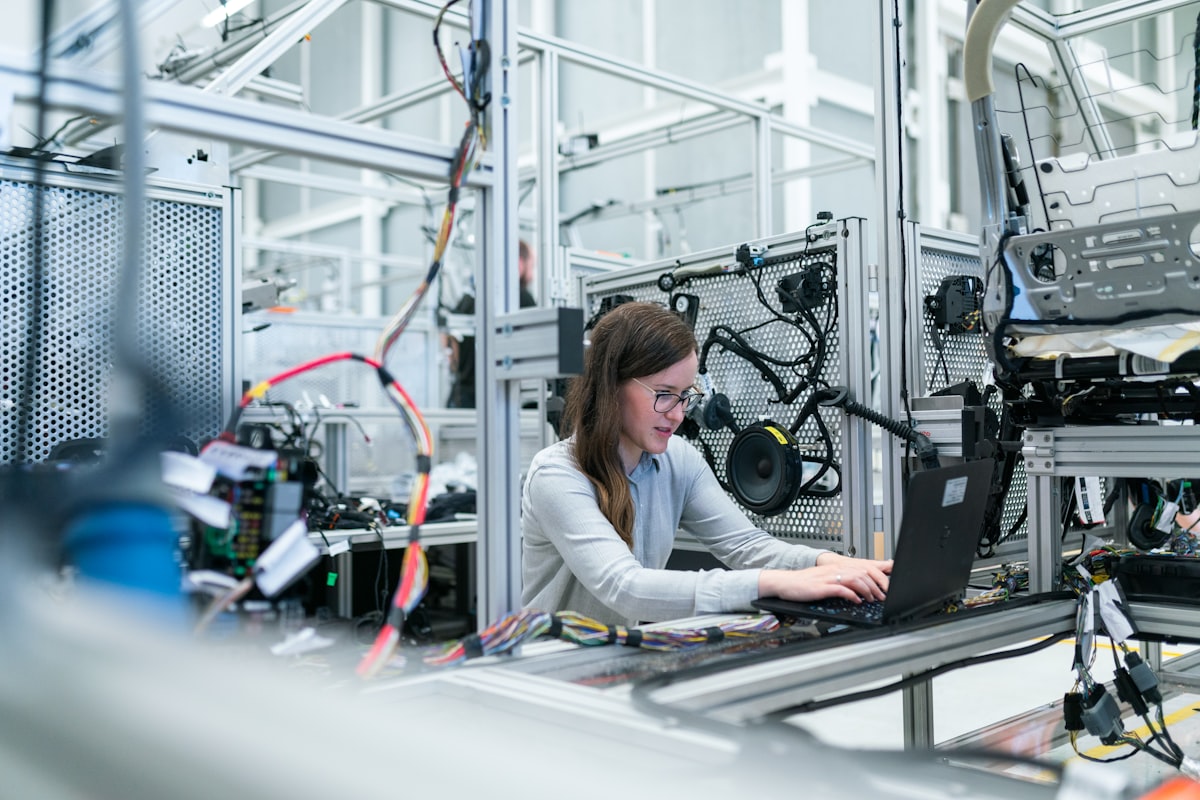
Engineered specifically around the demands of Food Processing.
In food and confectionery processing, hygiene and moisture management are inseparable. Steam from hot washdowns easily condenses on cold overhead pipes and ceilings, threatening food safety through dripping. At the same time, sugar and starch ingredients absorb moisture instantly. Humidity Solutions engineers sanitary dehumidifiers that ensure food safety and uniform quality.
Commercial Chocolate & Confectionery Plant
“Maintained 42% RH in the cooling and packaging tunnels, completely eliminating sugar bloom and reducing post-sanitation dry time by 65%.”
Moisture Challenges & Engineered Solutions
CRITICAL SECTOR CHALLENGES
Overhead Ceiling Condensation Drips
Thermal vapor condensing on cold ceilings and dripping onto open processing lines, creating serious biological contamination risks.
Sugar Bloom & Confectionery Sticking
Moisture dissolving surface sugars on chocolate, candies, and jellies, causing gray blooming and sticky, unsellable batches.
Extended Sanitation Drying Downtime
Facilities waiting hours for floors, walls, and conveyor belts to dry after washdowns before restarting production shifts.
OUR APPLIED SOLUTIONS
Sanitary Washdown Construction
Sloped internal drain pans and corrosion-proof components preventing stagnant water pooling inside the machinery.
Rapid Post-Washdown Dehumidification
High-volume air turnover drying production halls within 45 minutes of washdown, drastically reducing operational downtime.
Low-Temperature Operation
Effective water extraction down to 4°C for meat cutting rooms, cold curing cellars, and spiral freezer entry points.
RECOMMENDED EQUIPMENT
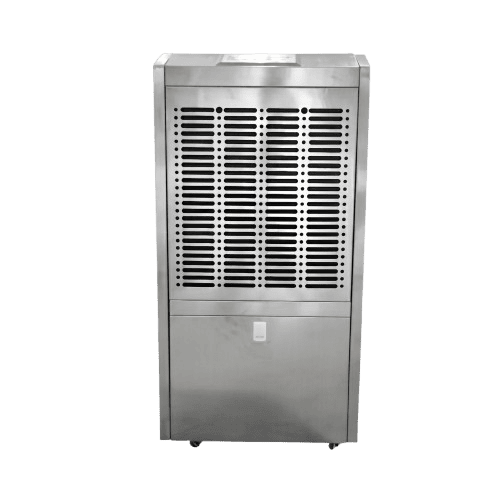
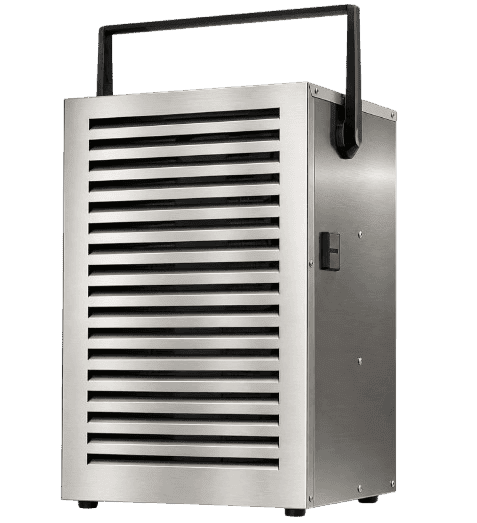
Pre-configured for the airflow, thermal load, and drainage requirements typical of food processing environments.
Explore Other Applications
LET'S FIND THE RIGHT
HUMIDITY SOLUTION.
“Tell us about your space, application and humidity requirements.”
AMFAH INDIA TRADING PVT LTD.
Specialized engineering and distribution of premium dehumidifiers, air purifiers, and industrial climate-control systems.
153/C, Oshiwara Industrial Centre Premises CHS Ltd,
Near Link Road, Opp. Oshiwara Bus Depot,
Goregaon (West), Mumbai - 400104
Dedicated Technical Support & Consultation